Enclosed Batching Plant Conveyors: Layout and Access
Quick Answer: Why Plan Enclosed Conveyor Layouts Early?
Enclosed conveyor layouts should be planned early because aggregate transfer points affect dust control, material spillage, belt maintenance, site cleanliness, and environmental approval. A well-planned conveyor route helps protect concrete batching plant stability while keeping daily inspection and cleaning practical.
Buyers should review conveyor direction, cover design, transfer height, maintenance access, dust collection, drainage, and emergency stop positions before the plant layout is finalized.
Enclosed Conveyor Planning Table
| Planning Area | What to Check |
|---|---|
| Conveyor route | Keep the belt route efficient while avoiding truck lanes, drainage channels, and service conflicts. |
| Cover design | Confirm dust protection, weather protection, access panels, and safe inspection points. |
| Transfer points | Plan chutes, skirts, cleanup access, and guards to reduce spillage and dust. |
| Maintenance access | Leave room for belt adjustment, roller replacement, cleaning, and emergency service. |
| Safety controls | Check emergency stops, guards, walkways, lighting, and operator visibility. |
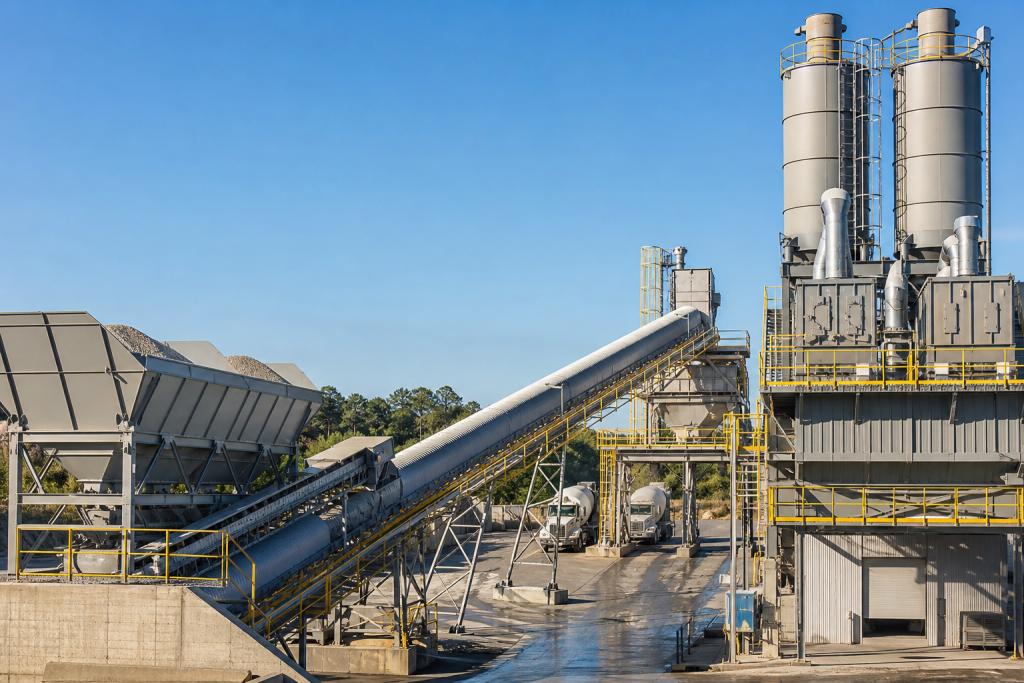
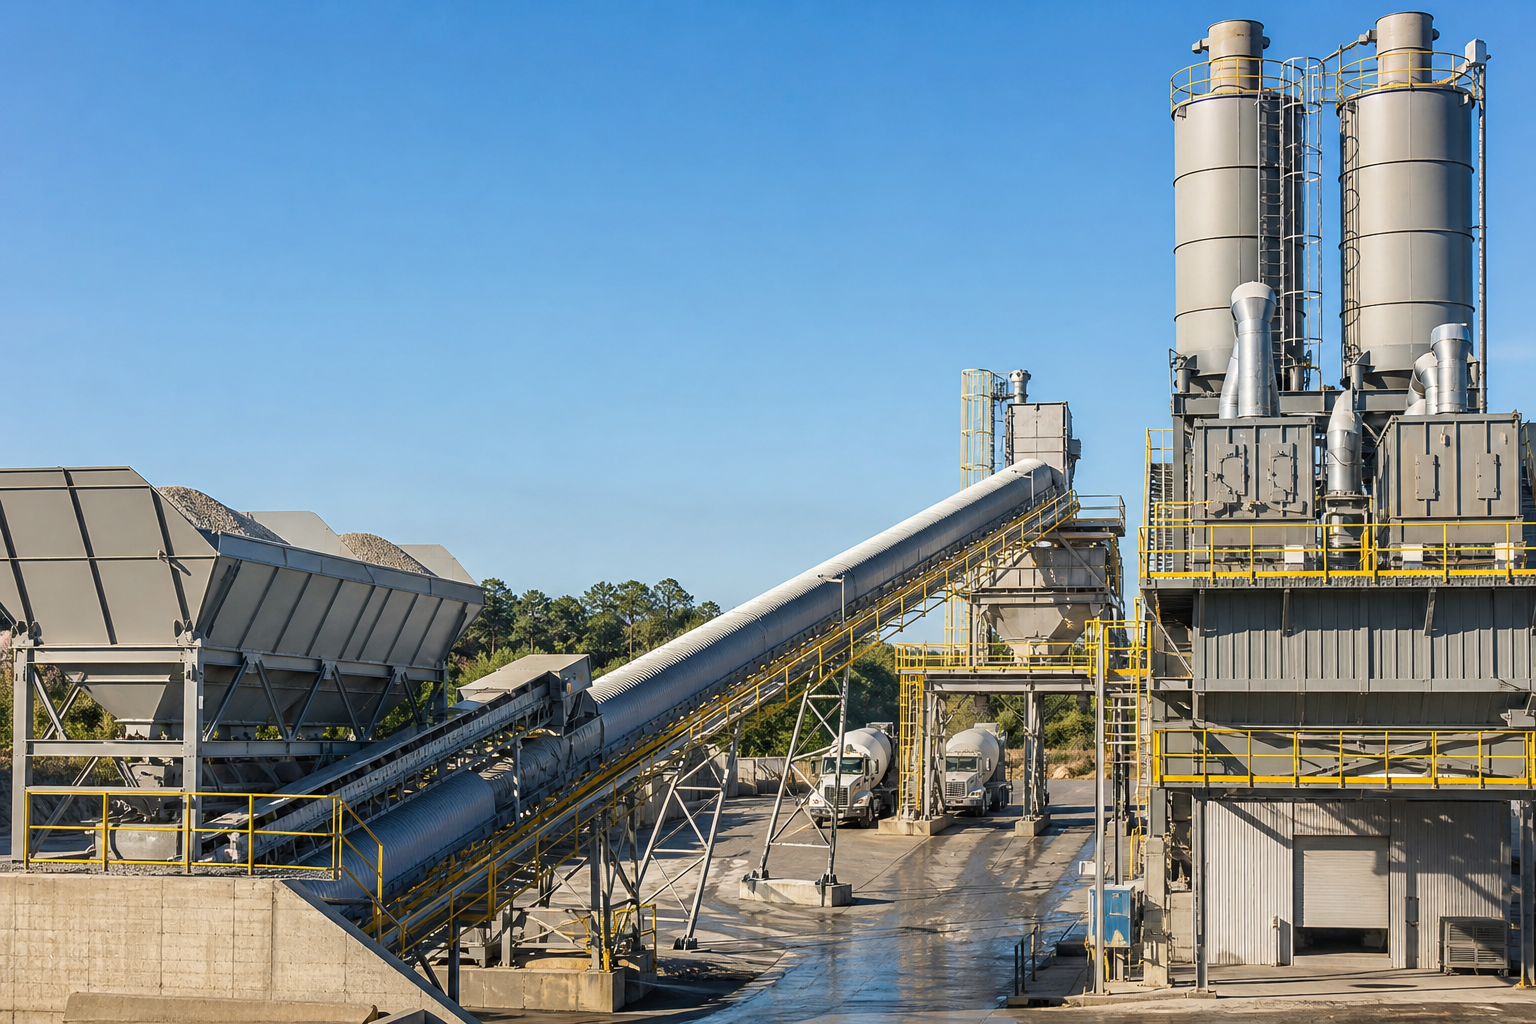
Enclosed batching plant conveyor planning should balance material routing and dust control with guarding, cleaning access and isolated maintenance. Review transfer points, inspection doors, platforms and traffic conflicts before approving the layout.
This practical equipment-planning guide is supported by the primary technical references cited below. Apply the project specification, equipment instructions and local environmental and occupational requirements; the cited guidance does not establish approval or verified performance for this plant.
Review the conveyor route and maintenance access together
A stationary concrete batching plant or mobile concrete batching plant is often compared by rated output, mixer model, aggregate bin capacity, cement silo quantity, control system, and installation footprint. Those specifications remain important. The layout review should also define the physical route from aggregate storage to weighing, mixing and truck loading.
Open transfer points and exposed conveyors can still work in the right environment, but they may add cleaning work, expose moving components to weather, and make dust-control planning more dependent on operator routines. Enclosed conveyor sections, covered transfer points, and well-placed dust-control equipment can help the plant team manage material flow with fewer interruptions and a cleaner working area.
Enclosures need service access, not just covers
A conveyor enclosure is only useful if the plant team can inspect, clean, and service the equipment inside it. Inspection doors, removable panels, guarded access points, walkways, lighting, and safe working clearances should be reviewed during layout planning. If service access is treated as an afterthought, a cleaner-looking conveyor can become harder to maintain.
For U.S. concrete construction, OSHA 1926.702(j) requires potentially hazardous energy sources to be locked out and tagged during maintenance or repair when inadvertent operation could cause injury. Review how the selected conveyor is isolated before hands-on service or access behind guards. An emergency-stop button, inspection door or removable cover does not substitute for the approved isolation and guarding procedure. OSHA 29 CFR 1926.702(j): Lockout/Tagout Procedures.
For compact mobile plants, use serviceable covers and guarded access points that can be handled under the equipment instructions and required isolation procedure after transport and setup. For larger ready-mix plants, it may mean longer inspection platforms, fixed dust-collection ducting, protected cable trays, and transfer-point enclosures that do not interfere with mixer loading or truck movement. The correct design depends on plant type, output target, aggregate condition, site footprint, and maintenance staffing.
Transfer points deserve early planning
Many dust and cleanup issues begin where material changes direction: under an aggregate bin, at a belt transfer, above a weighing hopper, or at the mixer feed point. These areas may need skirts, chute liners, sealing strips, dust collector connections, inspection doors, and enough space for cleaning tools. They also need a practical route for technicians to reach them without stepping into truck traffic or blocking production.
Good transfer-point planning can also support more stable aggregate feeding. If material drops cleanly, belts track properly, and buildup is easier to remove, operators are less likely to face avoidable stoppages. The result is not only a cleaner plant, but also a more predictable batching rhythm for the concrete mixer.
Dust-control equipment should match the material route
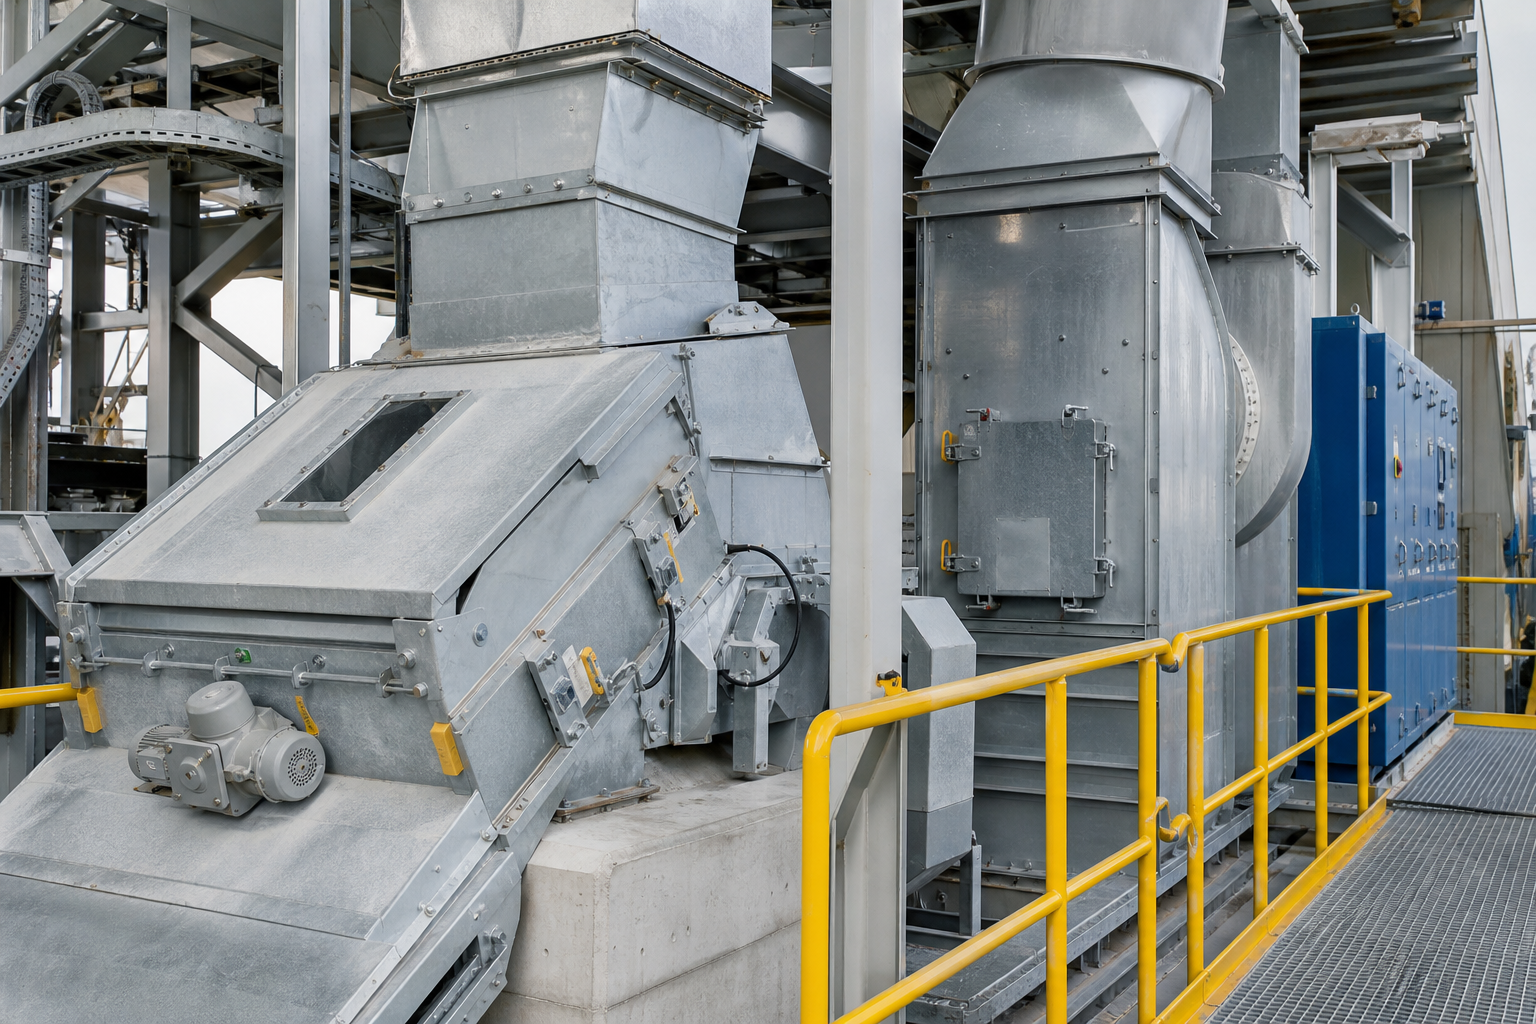
Dust-control equipment works best when it follows the actual material route. A dust collector positioned near a silo vent does not solve every transfer-point issue, and a covered conveyor does not remove the need to review where air, fines, and vibration will move during operation. Equipment buyers should discuss the aggregate route, cement handling, mixer feed point, and cleaning routine together.
In some plants, the priority may be enclosed aggregate conveyors and sealed transfer chutes. In other layouts, it may be dust collector access, silo vent maintenance, mixer charging control, or cleaner truck loading areas. A practical plan balances enclosure, ventilation, inspection access, safety, and cost.
Cleaning time affects production planning
Cleaning routes are often less visible than mixer size or conveyor length, but they affect daily output. If operators can clean around bins, belt return areas, transfer chutes, and mixer access points without moving around obstacles, maintenance becomes part of the normal shift routine. If cleanup is difficult, small material spills can become larger reliability issues.
For covered U.S. general-industry tasks, OSHA 1910.1053(h) restricts cleaning methods that could contribute to respirable-crystalline-silica exposure, including dry sweeping and compressed-air cleaning, with stated exceptions. Define the cleaning method together with the applicable exposure-control and equipment-isolation procedures. Construction work has a separate silica rule; convenient access does not make every cleanup method acceptable. OSHA 29 CFR 1910.1053: Respirable Crystalline Silica.
Clean material routing also helps supervisors inspect the plant. When dust and spilled aggregate are controlled, unusual buildup, belt misalignment, damaged skirts, blocked chutes, and air leaks are easier to notice. That supports earlier maintenance decisions before a small issue stops production.
Downstream equipment feels upstream variation
Material handling is upstream from truck loading, but the effects can be seen across the supply chain. Mixer trucks may wait if a transfer point needs cleaning. A concrete pump may receive concrete less smoothly if truck arrival times become irregular. Project supervisors may need more communication with the batching operator when production rhythm changes. For this reason, conveyor enclosure and dust-control planning should be treated as part of the full production workflow.
Buyers can use the product center to review concrete batching plant and equipment options, then discuss aggregate bin layout, conveyor routing, enclosure requirements, dust-control equipment, mixer feeding, and service access with hengyuan Concrete Machines before finalizing a project plan.
Practical checklist for enclosed conveyor planning
- Review aggregate bin discharge, conveyor routing, transfer chutes, dust-control points, and mixer feeding together.
- Use covers, skirts, and enclosures where they improve dust control without blocking inspection or cleaning.
- Place inspection doors, access panels, platforms, and cable trays where service teams can reach them safely.
- Plan dust collector ducting and filter access around the actual material route, not as a separate late-stage item.
- Keep cleaning routes clear around bin outlets, return belts, transfer points, weighing hoppers, and mixer access areas.
- Protect conveyor drives, sensors, wiring, and moving parts from unnecessary dust, water, impact, and vibration.
- Include truck loading, pump supply, traffic flow, and maintenance access in the plant layout discussion.
FAQ
Why should concrete batching plant buyers review enclosed conveyor layout early?
Conveyor routing affects dust control, material cleanup, transfer-point inspection, maintenance access, mixer feeding, and site traffic. Reviewing it early helps the equipment plan fit the working site.
Do enclosed conveyors remove the need for cleaning?
No. Enclosures can reduce exposure and improve control, but operators still need inspection doors, cleaning access, and service routines around transfer points, belts, and hoppers.
Where should dust-control planning start?
Start with the material route: aggregate bins, belt transfers, weighing hopper, mixer feed, cement silo vents, and truck loading area. Dust-control equipment should match where material and air actually move.
What should buyers prepare before discussing conveyor enclosure requirements?
Useful details include aggregate types, expected capacity, site footprint, bin layout, conveyor route, mixer model, dust-control expectations, truck loading plan, cleaning routine, and service access requirements.
Conclusion-Concrete Batching Plant Planning Checklists
Enclosed conveyor planning should connect material routing, dust controls, guarding, isolation and service access with the actual production workflow. A useful plan connects aggregate storage, covered conveyors, transfer-point design, dust-control equipment, service walkways, mixer feeding, truck movement, and maintenance routines. Buyers can contact hengyuan Concrete Machines with project details to discuss concrete batching plant configuration, material routing, and service planning.
Our Whatsapp: +86 199 3949 4756